HDPE Mining Pipe: The Ultimate Solution for Australia's Rigorous Mining Demands
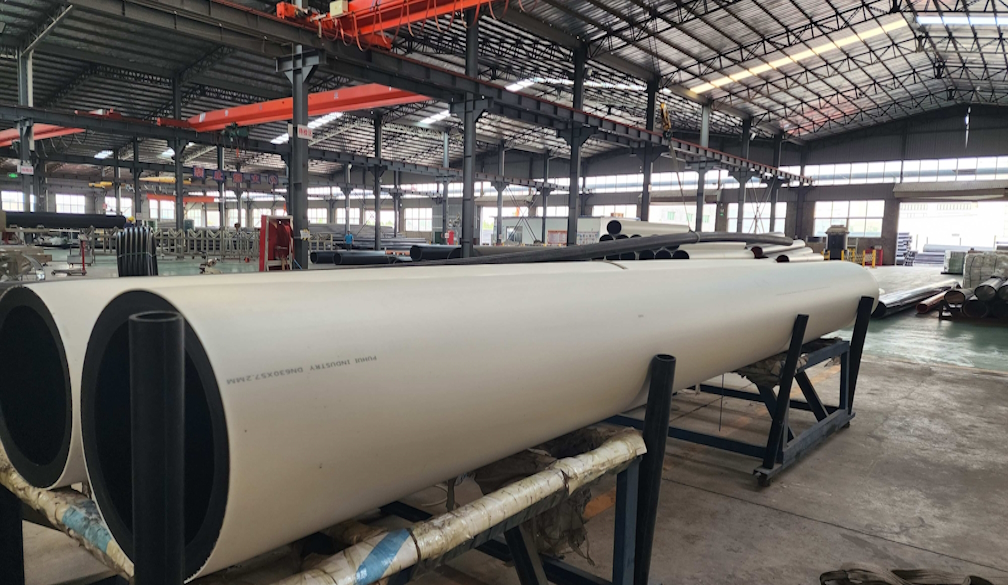
In the heart of Australia's mining sector—from the iron-rich red dust of the Pilbara to the complex underground networks of New South Wales—The piping infrastructure you choose directly impacts how efficiently you work, how safe your site is, and how well you manage environmental responsibilities." High-Density Polyethylene (HDPE) mining pipe has long been the industry's gold standard, offering unparalleled resistance to corrosion, abrasion, and chemical attack. However, as mine sites face increasingly extreme conditions, a new generation of engineered piping is setting a higher benchmark: HDPE Co-Extruded Piping Systems.
The Evolution of HDPE Mining Pipe
Modern mining operations demand more than just basic durability. They require a piping system that is capable of handling high-pressure slurry transport, aggressive mine water dewatering, and critical fire protection services across vast and inaccessible terrains. Traditional steel pipes fall short due to its corrosion and high maintenance costs, while standard HDPE pipes , can struggle with thermal stress and UV degradation when exposed to Australia's unforgiving sun.
This is where advanced co-extrusion technology transforms the landscape. By manufacturing pipes with a co-extruded layer, manufacturers create a dual-structure product that combines the proven strength of a PE100 inner core with a specialized outer functional layer. This synergy of materials delivers a performance that is greater than the sum of its parts, making it the preferred choice for both surface and underground mining applications.
Spotlight on HDPE Co-Extruded White Layer Pipe
"When you get down to the specifics, it's the HDPE Co-Extruded White Layer Pipe that Australian mine operators are really getting excited about."It is specifically engineered to address the unique climatic and operational challenges of the region.
Beating the "Outback Sun" Effect.
Australia’s intense solar radiation is a formidable adversary for piping infrastructure.
Thermal Management: The reflective white outer layer minimizes solar absorption. This keeps the pipe's surface temperature significantly lower than standard black HDPE pipes. By reducing heat build-up, the pipe avoids the pressure de-rating that typically plagues black pipes in summer, allowing for the use of thinner pipe walls and delivering substantial material cost savings without compromising on flow capacity.
Reduced Thermal Expansion: Lower operating temperatures translate to reduced linear expansion. This simplifies installation design by decreasing the need for extensive "snaking" layouts to accommodate movement, leading to faster and more cost-effective installations.
Superior UV Resistance and Longevity
Exposure to UV rays causes embrittlement and degradation in standard polymers. The co-extruded white layer incorporates advanced UV stabilizers directly into the outer skin during manufacturing. This provides a robust barrier against UV penetration, ensuring the structural integrity of the pipe for decades, even when installed entirely above ground.
Enhanced Abrasion Resistance for Slurry Transport
The inner core of the co-extruded pipe can be optimized for slurry applications. When combined with the protective outer layer, mine operators benefit from a pipe that offers exceptional resistance to the abrasive wear caused by high-velocity mineral slurries, while the outside withstands the harsh elements. This dual protection drastically extends the service life of the pipeline and reduces unplanned downtime.
PUHUI INDUSTRY: FM-Approved Confidence for Mining Projects
When specifying HDPE piping for critical mining infrastructure—particularly for underground fire protection and high-stakes process lines—certifications are non-negotiable. PUHUI INDUSTRY stands at the forefront of the industry, offering comprehensive HDPE piping solutions backed by world-class certifications that give Australian engineers and EPC contractors complete peace of mind.
A key differentiator for Puhui Industry is its FM Approval certification. FM Approvals (Factory Mutual) is one of the most respected global testing laboratories. FM Approval Standard 1613 signifies that the HDPE products have undergone rigorous, independent testing for toughness, pressure endurance, and performance in demanding fire protection applications.
Why FM Approval Matters in Australian Mining
Uncompromising Safety: For underground mining operations, fire protection is paramount. FM-approved HDPE pipes ensure that safety systems remain operational under extreme duress, providing a certified level of reliability that is critical for personnel safety and asset protection.
Risk Mitigation: Using FM-certified components demonstrates a commitment to the highest standards of quality control. This helps mining companies and contractors meet strict corporate governance, insurance, and compliance requirements.
Global Standard, Local Trust: For international EPC contractors working in Australia, the FM mark provides an instantly recognized guarantee of quality, simplifying the procurement process and ensuring that the specified materials meet rigorous international performance benchmarks.
Conclusion: Future-Proofing Australia's Mining Infrastructure
The shift towards HDPE Co-Extruded White Layer Pipe represents a strategic evolution in mining infrastructure. It is a technology that not only solves the immediate challenges of abrasion and corrosion but also proactively addresses the environmental stressors which is unique to Australia.
By partnering with a certified manufacturer like PUHUI INDUSTRY, which combines innovative co-extrusion technology with the safety assurance of FM Approval, mine operators are making a long-term investment in operational efficiency, cost reduction, and workplace safety. For your next mining project, from dewatering to slurry transport, the proven performance of co-extruded HDPE piping is the foundation upon which reliable and sustainable operations are built.
To sum it up , mining is about endurance. Your piping infrastructure should be no different. With HDPE Co-Extruded White Layer Pipe, you're not just getting a product that withstands the Australian sun and the relentless grind of slurry transport; you're getting a system engineered for decades of dependable service.
And when that pipe carries the FM Approval mark from PUHUI INDUSTRY, you're backed by more than just advanced manufacturing—you're backed by independent, world-class verification that your safety systems will perform when it matters most.
So, whether you're planning a new dewatering line, upgrading your tailings network, or specifying fire protection for an underground expansion, make the choice that keeps your operation running—shift after shift, year after year.

 Blackhawk Network VP Head of ANZ Kieran Nolan