Maximising Production Efficiency in Australian FMCG Manufacturing Through Strategic Equipment Upgrades
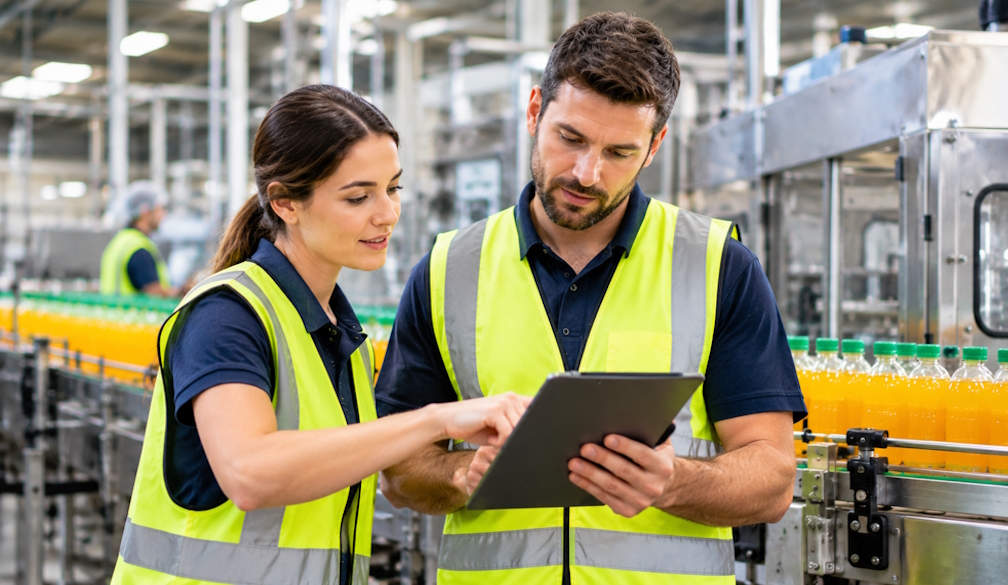
As a cornerstone of the national economy, the Australian manufacturing sector employs nearly 870,000 workers, heavily driven by food, beverage, and chemical production. However, Fast-Moving Consumer Goods (FMCG) manufacturers are facing unprecedented margin pressures. Volatile energy markets, labour constraints, and global supply chain vulnerabilities have drastically transformed the industrial landscape. A recent parliamentary inquiry report emphasised the urgent need to establish technologically advanced, strategically positioned manufacturing facilities to insulate the Australian supply chain from global economic shocks. To remain competitive, facility managers are shifting their focus away from offshore reliance and towards optimising their local capabilities. The key to this successful transition lies in targeted, strategic equipment upgrades that streamline production lines and dramatically cut down on wasted time and energy.
Targeting Bottlenecks with Advanced Mixing and Processing
In food, beverage, and chemical plants, fluid mixing and blending are often the most time-consuming steps in the entire production cycle. Legacy agitators and rudimentary blending tanks frequently struggle with high-viscosity liquids or the rapid dispersion of stubborn powders into fluids. These mechanical bottlenecks result in extended batch times, inconsistent product quality, and higher electricity usage per unit produced.
Addressing these specific pinch points requires implementing specialised, modern engineering solutions. Upgrading to advanced industrial fluid mixing technology can drastically reduce the time it takes to incorporate bulk materials. For example, implementing solutions from local experts like mixquip allows facility managers to seamlessly incorporate bulk materials without the long processing times associated with older equipment. By deploying highly engineered, high-shear systems, facilities can achieve much faster output rates while simultaneously lowering their overall energy expenditure.
The Pressures Forcing a Manufacturing Makeover
The financial reality for local manufacturers is becoming increasingly complex. According to data from the Australian Bureau of Statistics, manufacturing input prices rose by 10.7% over a recent twelve month period. This surge was primarily driven by unstable energy and fuel costs. Furthermore, gas prices for Australian industry have spiked by over 40% since 2022. For energy-intensive sectors like food processing and chemical manufacturing, these numbers represent a significant threat to long-term profitability.
Coupled with material delays reported by over 60% of local manufacturers, internal operational efficiency is no longer just a lofty goal. It is a strict operational necessity. Deciding if your manufacturing company needs a makeover often starts directly on the factory floor, where assessing legacy systems can reveal hidden inefficiencies. Modernising outdated machinery is one of the fastest and most reliable ways to insulate a facility from external price shocks and material shortages.
Key Areas for Operational Optimisation
Replacing old equipment is an investment that now boasts a significantly compressed financial payback period. Thanks to rising input costs and modern engineering efficiencies, payback horizons have shifted from multi-year wait times to near-term returns. When planning facility upgrades, FMCG manufacturers should focus on several high-impact areas:
- High-efficiency processing units: Upgrading to modern fluid mixers and agitators ensures rapid dispersion of ingredients. This can effectively halve batch processing times and significantly boost daily yield without requiring extra floor space.
- Energy-saving motor integration: Transitioning to green heat and electric-powered mechanical processes protects businesses from fossil fuel volatility. A Smart Energy Council report highlighted that modernising energy-hungry facility equipment can yield incredible savings. A notable Mars Petcare facility achieved a 30 to 40% net reduction in energy costs simply by upgrading to high-efficiency alternatives.
- Automation and touchless workflows: Integrating smart sensors and automated dosing systems limits human error, reduces product waste, and ensures strict quality control across every single batch.
- Intelligent hybrid models: By optimising local production lines, brands can prioritise sovereign manufacturing capabilities for core products. This eliminates the hidden expenses of expedited international shipping and costly offshore stockouts.
Seizing Funding and Future-Proofing
To support these critical upgrades, the Federal Government and various industry bodies are stepping in with substantial backing. Initiatives like the 15 billion dollar National Reconstruction Fund are actively investing in value-adding agriculture and manufacturing priorities. Major FMCG players are already leveraging debt financing and grants to modernise their factory floors. Furthermore, the Advanced Manufacturing Growth Centre and the Industry Growth Program provide targeted advisory services and commercialisation funding to help small to medium enterprises boost their supply chain resilience.
Additionally, Australia's Food and Beverage Accelerator works directly with local businesses to integrate advanced manufacturing techniques and adopt sustainable processing methods. Ultimately, surviving in the current Australian economic climate requires agility and foresight. By embracing strategic equipment upgrades and modernising core production lines, FMCG manufacturers can transform their operations from energy-draining liabilities into highly efficient, future-proofed assets.

 Business Daily Media